WhatsApp:+86 18005022363 WeChat: +86 18005022363
 Email:
Description
Application Scenarios
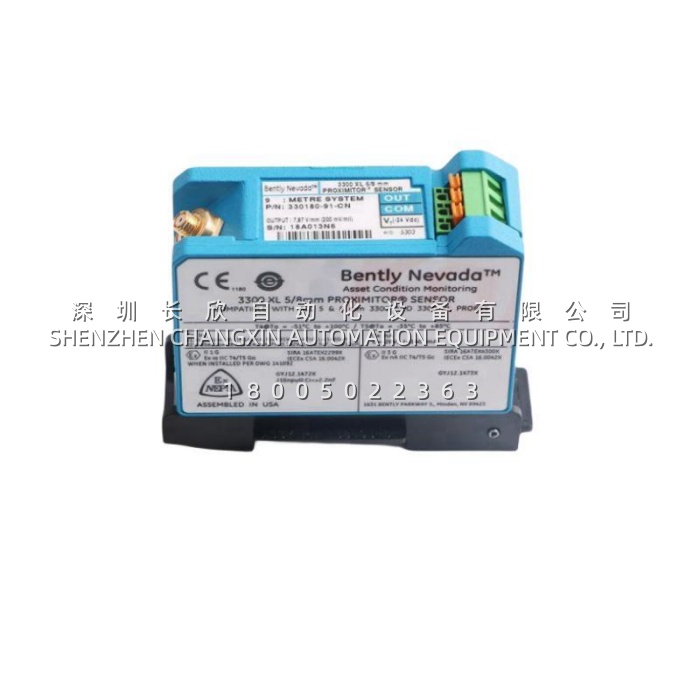
In a centrifugal air compressor package operating in a petrochemical facility, the rotor generates substantial axial thrust during high-speed rotation. Should the thrust bearing begin to wear, the rotor will shift along its axis—potentially causing catastrophic blade-to-casing contact if left undetected . The Bently Nevada 991-06-50-01-01 addresses this critical concern by providing a live thrust position signal directly to the machinery control system. By converting the differential gap measurement from a pair of 3300 NSv proximity probes into a standard 4-20 mA loop signal, the 991-06-50-01-01 enables operators and protection systems to detect early thrust bearing degradation and initiate timely intervention before mechanical damage occurs .
Parameter
| Parameter | Value/Description |
|---|---|
| Product Model | 991-06-50-01-01 |
| Manufacturer | Bently Nevada |
| Product Category | Thrust Transmitter Module |
| Full-Scale Range | 0.6-0-0.6 mm (±0.6 mm axial displacement) |
| System Length | 5.0 meters (16.4 feet) |
| Mounting | 35 mm DIN-rail clips |
| Agency Approval | CSA Division 2 |
| Input Compatibility | 1 × 3300 NSv Proximity Probe + extension cable |
| Output Signal | 4-20 mA DC, 2-wire loop-powered |
| Power Supply | +12 to +35 V DC at transmitter terminal |
| Loop Accuracy | ±1.5% of full scale (typical) |
| Operating Temperature | -35°C to +85°C |
| Storage Temperature | -51°C to +100°C |
| Weight | 0.43 kg (0.9 lbm) |
Technical Principles and Innovative Values
Innovation Point 1: Integrated Proximitor Design. Traditional thrust monitoring architectures required a separate proximitor unit mounted between the probe and the control system, consuming panel space and introducing additional wiring connections. The 991-06-50-01-01 integrates the Proximitor sensor function directly within the transmitter housing, eliminating this intermediary component and simplifying the entire measurement chain . This integrated approach reduces installation complexity, minimizes potential failure points, and lowers overall system cost.
Innovation Point 2: Robust “Not OK” Diagnostic Circuitry. The 991-06-50-01-01 incorporates a sophisticated fault detection circuit that continuously monitors probe integrity and signal validity. Should a probe cable break, a probe fail, or a signal become unreliable, the transmitter immediately drives its output below 3.6 mA within 100 microseconds, alerting the control system to disregard the measurement . This rapid fault signaling prevents dangerous false readings that could trigger unnecessary shutdowns or, worse, mask genuine machinery distress.
Innovation Point 3: CSA Division 2 Certification. The “-01” agency approval suffix designates CSA Division 2 certification, permitting installation in classified hazardous areas where flammable vapors or gases may be present under abnormal conditions . This certification is particularly valuable in petrochemical, oil and gas, and chemical processing facilities where control cabinets and junction boxes often reside in classified zones .
Innovation Point 4: Two-Wire Loop-Powered Simplicity. Operating on a standard 4-20 mA current loop, the 991-06-50-01-01 draws its operating power from the same two wires that carry its measurement signal . This loop-powered architecture eliminates the need for separate power supply wiring, reduces cable requirements, and simplifies integration with PLC, DCS, and machinery protection system analog input cards .